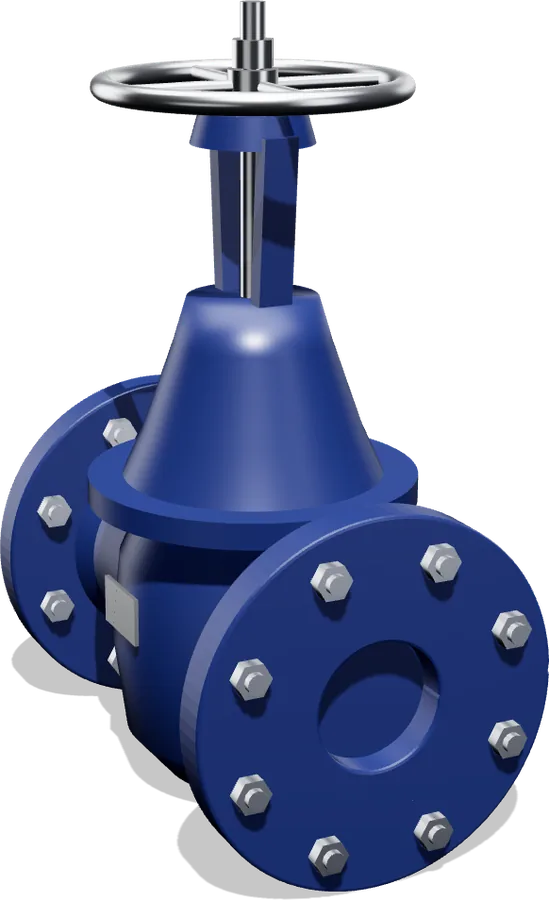
Why sequence matters
A gasket seals only when it is compressed evenly all the way round. Tightening bolts one after another around the circle pulls the flanges together on one side first, tilting them. The last bolts then cannot close the gap evenly, and the joint leaks under pressure or temperature.
The star (cross) pattern
Tighten bolts in a cross pattern, moving to the opposite side of the flange each time. On an 8-bolt flange, a common sequence is:
1 · 5 · 3 · 7 · 2 · 6 · 4 · 8
where bolt 5 sits opposite bolt 1, and so on. Number the bolts with chalk before you start.
Tighten in stages
- Snug: hand-tighten all nuts so the flanges sit parallel. Check the gap is even.
- Pass 1: about 30% of target torque, in the star pattern.
- Pass 2: about 60% of target torque, in the star pattern.
- Pass 3: 100% of target torque, in the star pattern.
- Final check: one pass round the circle at 100% until no nut turns further.
Always use the torque values from your site procedure or the gasket manufacturer. ASME PCC-1 is the widely used guideline for bolted flange joint assembly.
Before you tighten
- Use a new gasket every time. Compressed gaskets do not reseal.
- Check the gasket type and rating match the flange class and facing.
- Inspect the flange faces for scratches across the serrations.
- Lubricate the stud threads and nut faces so torque turns into bolt load.
- Use the correct stud grade, for example ASTM A193 B7 with A194 2H nuts for carbon steel service.